Engineering Guide · 5 min read
316 Stainless Steel Fasteners: Applications, Grades and Service Limits
316’s molybdenum content helps resist localized corrosion. Sea air, immersion, 316L and the fastener’s strength class each change the selection.
The short answer: 316 stainless steel is a common choice for coastal fittings and process equipment where chloride exposure matters. Its molybdenum content helps resist localized corrosion, but a bolt exposed to sea air and one permanently submerged in seawater face very different conditions.[1][2][3]
Explore the stainless steel guide series
These guides cover the material basics and the 304/316 choice:
- What Is Austenitic Stainless Steel? A Fastener Buyer's Guide — material structure, cold work and grade selection.
- 304 Stainless Steel Fasteners: When to Use Them and What to Specify — the starting grade for general-purpose assemblies.
- 304 vs 316 Stainless Steel Fasteners: What the Data Says — when the exposure justifies choosing 316.
316, 316L and A4
316 is an austenitic chromium-nickel-molybdenum stainless steel. Molybdenum improves resistance to pitting and crevice corrosion in chloride-bearing environments.[1][2]
| Description | Meaning |
|---|---|
| 316 / S31600 | The alloy identity; finished-fastener strength is a separate requirement. |
| 316L / S31603 | The low-carbon version of the alloy. |
| A4-70 or A4-80 | An ISO fastener grade and strength class. A4 covers a chemistry range, so name 316 or 316L separately when required. |
316L reduces welding-related carbide precipitation and intergranular-corrosion risk. Its resistance to pitting and crevice corrosion is generally similar to 316’s; choose it for the part’s fabrication requirements rather than as a general chloride-resistance upgrade.[1][2]
Sea air, seawater and wet crevices
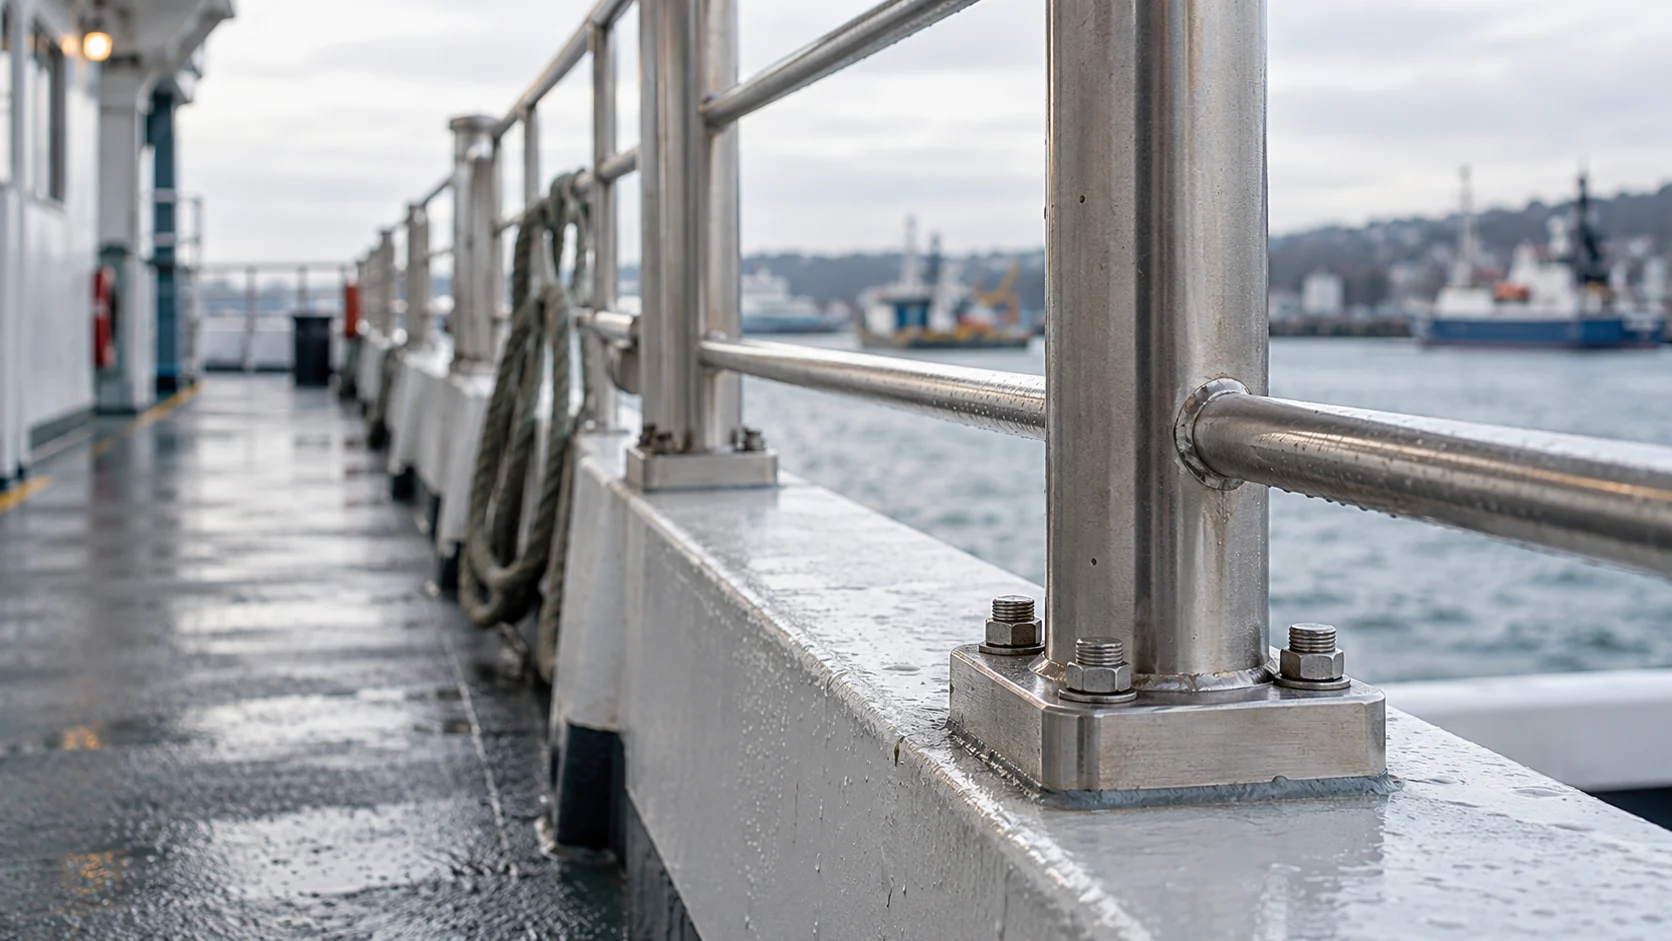
316 is used in coastal, chemical, pharmaceutical and food-processing equipment. A washed external frame, a splash zone and a gasketed flange expose their fasteners differently.[1][2]
Under a washer or bolt head, retained liquid can lose oxygen while chlorides concentrate. That crevice may be more aggressive than the exposed surface. “Marine grade” is a commercial description, not an immersion rating.[3][4]
| Service condition | Selection decision |
|---|---|
| Coastal air or occasional salt spray | 316 is a candidate where the joint drains and salt deposits can be removed. |
| Sheltered joints, deposits or retained water | Review the crevice geometry, cleaning access and retained liquid. |
| Continuous seawater contact or stagnant brine | Obtain a documented alloy and joint recommendation before approving 316. Water quality, flow and temperature matter; a more resistant alloy may be needed. |
| Warm chlorides or evaporating deposits | Assess concentration, temperature and tensile stress together, including stress-corrosion-cracking risk. |
Cleaning and shutdown can change the exposure. Residual liquid and evaporating deposits can become more concentrated than the normal process stream.[3][4][5]
Strength and the finished fastener
Cold work raises the strength of austenitic stainless. An annealed material datasheet is therefore a poor guide to a cold-worked bolt’s strength.[2][6]
For metric fasteners with full tensile loadability, ISO 3506-1:2020 specifies minimum tensile strengths of 700 MPa for A4-70 and 800 MPa for A4-80, evaluated at 10–35 °C. Some head designs have reduced loadability. These are mechanical requirements, not allowable joint loads; the stainless fastener markings guide covers the classes in detail.[6][7]
For inch bolts, hex cap screws and studs within its scope, ASTM F593-24 Group 2 permits 316 and 316L. Name the alloy and condition on the order.[8]
Pressure-equipment drawings may specify bolting to ASTM A193/A193M-26. Follow the drawing’s grade and class; the Grade B8M guide covers that 316-type route.[9]
The rest of the joint
Match the nut’s mechanical requirements to the bolt, as well as its thread and alloy. ISO 3506-2:2020 covers stainless nut properties, including proof load.[10]
A wet connection to aluminum or galvanized steel can accelerate corrosion of the more active metal. Have the connection designer approve isolation and drainage details that preserve load transfer and avoid trapping liquid. Paint alone is unreliable insulation where tightening damages it.[11]
Assembly and surface condition
316 threads can gall during tightening. Use clean, undamaged threads and an identified lubricant or factory treatment suited to the process. Adding anti-seize while retaining a dry-thread torque can produce excessive preload. The thread galling guide explains the assembly controls.[12]
ASTM A967/A967M-25 offers chemical-passivation treatments and verification tests, particularly for contaminant-iron removal. Name the required treatment and test on the order.[13]
Match the delivered lot to its chemical analysis and finished-fastener test reports.[14]
X-ray fluorescence (XRF) can help identify the alloy family through elements such as molybdenum, but cannot measure carbon. If testing is required to verify 316L’s carbon limit, use a carbon-capable method.[14][15]
References
- Outokumpu. Supra range datasheet. 316 and 316L identities, molybdenum-alloyed grades, fabrication and applications.
- Australian Stainless Steel Development Association. 316: The First Step Up. Alloy behavior, low-carbon variants, applications and cold-work strengthening.
- British Stainless Steel Association. Selection of 316, 304 and 303 types for seawater applications. Water quality, flow, temperature and crevice conditions affecting 316.
- Australian Stainless Steel Development Association. Crevices and Corrosion. Retained liquid, oxygen depletion and localized conditions beneath fasteners and gaskets.
- E. A. Geary, Health and Safety Laboratory. A review of performance limits of stainless steels for the offshore industry, ES/MM/10/11, issued January 20, 2011. Environmental variables and concentrating deposits.
- British Stainless Steel Association. Stainless steel fasteners. ISO 3506:2020 chemistry ranges and property-class requirements.
- ISO. ISO 3506-1:2020 — Bolts, screws and studs with specified grades and property classes. Metric scope, ambient-temperature evaluation and geometry-dependent loadability; confirmed in 2025.
- ASTM International. ASTM F593-24 — Stainless Steel Bolts, Hex Cap Screws, and Studs. Inch product scope, Group 2 alloys and mating-nut requirements in the public scope.
- ASTM International. ASTM A193/A193M-26 — Alloy-Steel and Stainless Steel Bolting. Public scope for high-temperature, high-pressure and other special-purpose bolting.
- ISO. ISO 3506-2:2020 — Nuts with specified grades and property classes. Nut mechanical properties and proof-load requirements; confirmed in 2025.
- Australian Stainless Steel Development Association. Technical FAQ 1: Galvanic/Dissimilar Metal Corrosion. Electrical contact, conductive liquids, joined metals and isolation.
- Australian Stainless Steel Development Association. Technical FAQ 5: Galling and its Control. Lubrication, torque, thread condition and mating materials.
- ASTM International. ASTM A967/A967M-25 — Chemical Passivation Treatments for Stainless Steel Parts. Treatment options, alternative verification tests and application limits in the public scope.
- Australian Stainless Steel Development Association. Technical FAQ 4: Testing for Grade Confirmation. Traceable records and selection of material-identification methods.
- Thermo Fisher Scientific. Analysis of Stainless Steel Testing Using the Niton Apollo Handheld LIBS Analyzer. Carbon measurement and XRF limitations.