Engineering Guide · 5 min read
How to Use a Thread Pitch Gauge: Metric and Inch Threads
Identify an unknown screw thread with a pitch gauge and caliper. Learn how to check leaf fit, distinguish close pitches, and record a useful identification result.
The short answer: open a leaf on the thread pitch gauge, rest its toothed edge along the screw thread, and check that it follows several consecutive grooves. Read the matching leaf in millimeters or threads per inch, then combine that result with the thread diameter and the correct thread system. A leaf that fits gives you the pitch; you still need other information to identify the replacement.[1][2]
The awkward cases are the ones that almost fit. A few teeth can look convincing while the wrong spacing becomes apparent farther along the leaf. This walkthrough covers ordinary external threads on bolts, screws, and studs. For the complete purchasing specification after identification, use How to Specify a Bolt.
Check which threads your gauge covers
A folding thread pitch gauge, also called a screw pitch gauge or thread comb, carries a different tooth spacing on each leaf. Check the markings on the case and leaves before starting: metric leaves show pitch in millimeters; Unified-inch leaves show threads per inch, or TPI.[1]
The thread form matters too. Metric and Unified gauges use a 60° profile; Whitworth gauges use 55°. Mitutoyo lists these as separate gauge families, including combination sets. Check the actual leaf list: a combined metric/inch gauge may omit pitches that a larger set includes.[3]
Have a caliper, good lighting, and a thread reference appropriate to the equipment beside you. If you are working on a pipe fitting or a tapered thread, use its manufacturer's identification procedure; the nominal size and sealing connection require additional checks.[2]
Measure the threaded shank first
Remove loose dirt and inspect the screw and gauge for damaged teeth. Work on a clean, intact section away from the incomplete threads at the tip. With the caliper's outside jaws, measure across the thread crests, square to the screw axis. Record the reading and its unit rather than rounding immediately to a familiar size.
The measured outside diameter helps narrow the candidates. It may differ from the nominal diameter because of manufacturing tolerances; wear can make identification less certain. Compare it with a suitable thread reference, then check the possible pitches. Head width and hex-key size are separate features.[2][4]
Fit the leaf across several threads
Start with a likely pitch from the diameter check, then compare neighboring leaves. Inspect the contact between the leaf and the thread against a light background:
- Open one leaf. Keep the others clear of the work so you can see the measuring edge.
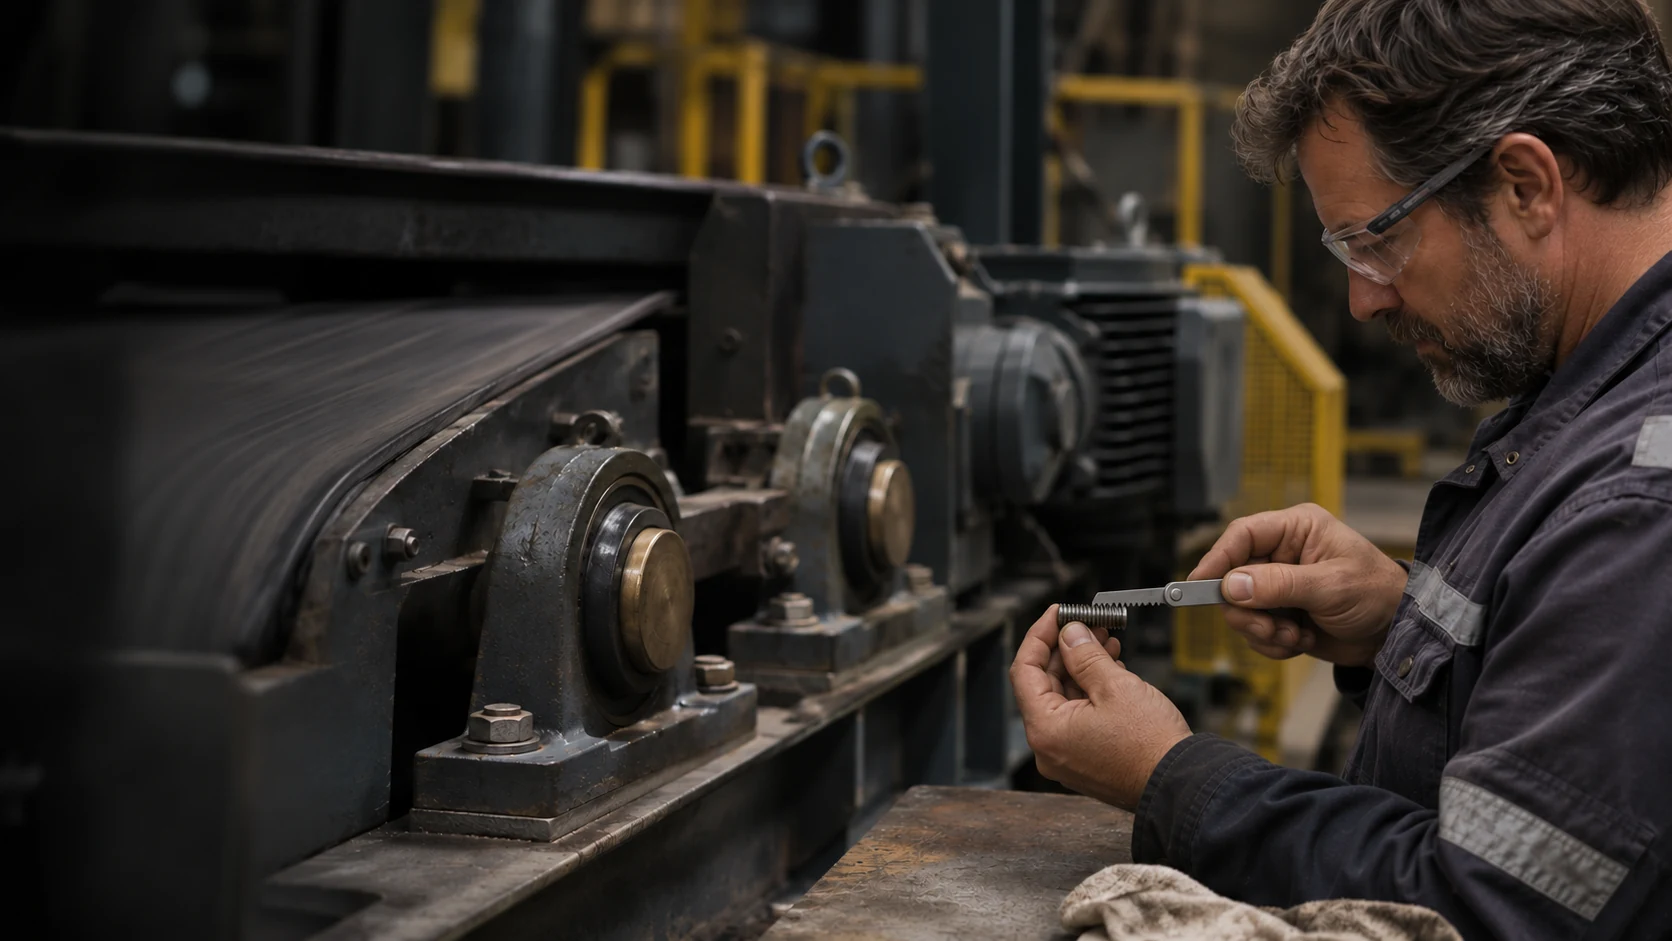
- Place it along the threaded shank. Let its teeth settle gently into several consecutive grooves. Keep the leaf aligned with the screw axis rather than angling it to make a few teeth fit.
- Hold the screw and leaf in front of a light source. Check the fit along the engaged edge. Gaps at the flanks or teeth that progressively ride out of the grooves suggest a mismatch. Try another leaf instead of pressing harder.
- Repeat and record. Lift the leaf, check another intact section, and write down the matching leaf's number, unit, and gauge family.[1][4]
If none fits, check the gauge's pitch range and thread family before deciding that the screw has an unusual thread. Dirt, local damage, or too little exposed thread can also prevent a clear reading. An uncertain fit is a reason to obtain a better sample or have the thread measured.
When metric and inch leaves seem to fit
A 20-TPI thread has a calculated spacing of 25.4 ÷ 20 = 1.27 mm. That is close to a 1.25 mm metric pitch: the difference is only 0.02 mm per interval. This explains why judging a short section by eye can be misleading. The 0.02 mm difference is not a thread-fit tolerance.[5]
Compare both leaves over as much sound thread as the gauge allows, then check the diameter and equipment documentation. If the visual comparison remains ambiguous, have the thread identified with suitable measuring equipment. The bolt-size callout guide explains how to write the result once the system is established.
Even identical diameter and TPI can leave two possibilities. YAMAWA identifies 1/4-20 as a size found in both Unified and Whitworth threads, whose profiles differ. On older equipment, confirm the thread family rather than assuming every inch thread is UNC or UNF.[5] For the subsequent choice between Unified coarse and fine threads, see UNC and UNF Threads.
A matching leaf is an identification result
A pitch gauge helps identify the spacing. Thread tolerance and functional fit require the inspection method specified for the part. Working thread ring gauges inspect external threads; working thread plug gauges inspect internal threads. These tools are selected for a particular thread size and class.[6]
For a nut or tapped hole, a narrow pitch-gauge leaf may reach the internal thread, provided you can see enough contact to judge it.[1] A crest-to-crest reading inside a nut is its minor diameter; compare it with an internal-thread reference rather than a bolt's outside diameter.[7] If the hole prevents a clear view of the leaf, use the drawing or have the internal thread checked by the supplier.
Send the measurement with the remaining questions
Keep what you observed separate from what still needs confirmation. An identification note can be short:
Illustrative identification note: “Removed socket head screw; outside thread diameter approximately 8 mm. A metric 60° gauge leaf marked 1.25 fits the accessible threads. Photos and sample available. Please confirm the thread designation against the mating part and drawing; material, strength grade, and finish remain to be specified.”
Attach a clear view of the whole fastener, the head markings, and the gauge contact. Add the measured length and where that measurement starts. Once the thread is confirmed, complete the product, material, finish, and quantity fields in the bolt specification guide. That gives the supplier both the evidence for identification and the requirements for the replacement.
References
- Starrett. Screw Pitch Gages. Leaf markings, thread families, and access to internal threads.
- Swagelok. Thread and End Connection Identification Guide, MS-13-77, Rev. H, February 2025, pp. 7–9. Diameter and pitch identification procedure; the guide's fitting-specific tables are not bolt acceptance criteria.
- Mitutoyo. Small Tool Instruments and Reference Gages, p. E-39, Series 188 and 950. Metric, Unified, and Whitworth leaf sets and their included pitches.
- paulimot. Determining the Metric Thread, step 3. Backlit comparison of gauge and thread.
- YAMAWA. Technical Tip No. 029: The Difference Between Unified Thread & Whitworth Thread. Coincident inch sizes and different profiles;
P = 25.4 / TPI. The 20-TPI comparison above is calculated from that relationship. - Vermont Gage. Thread Gages and Thread Classes and Setting Plug Gages. Working gauges, functional thread inspection, and selection by product thread class.
- Michigan Drill. Technical Data: Taps & Dies, glossary. Major and minor diameters of internal and external threads.